




Resin 3D printing by cotu s.r.o.: What really affects quality, accuracy, and production efficiency
How Stereolithography Works and Where Its Limitations Arise
Stereolithography (SLA and related projection technologies) is among the most precise methods of resin 3D printing. Its basic principle is selective curing of a liquid photopolymer using UV light (image projection) through the transparent bottom of the vat. Each layer of the model is cured separately, and the build platform then moves in a controlled manner along the Z axis, creating the final object layer by layer.
| Fig. 1 Principle of printing liquid materials - resins |
This principle makes it possible to achieve very fine details, a smooth surface and high dimensional accuracy, but also introduces technological limitations that are not apparent at first glance. The movement of the platform as it compresses the material into a layer creates mechanical and physical forces that directly affect the stability of the entire process.
If these phenomena are not properly controlled, they can result in microdeformations, variations in layer thickness or reduced overall 3D printing accuracy. For this reason, stereolithography cannot be viewed simply as “curing a layer”, but as a complex manufacturing process in which the details of control are decisive.
Overview of Projection Technologies
The main image projection technologies used in resin 3D printing include SLA, DLP, LCD and MJP, which differ in their curing principle, light source stability and suitability for long-term operation.
| Fig 2. Stereolithography technology |
SLA (laser stereolithography) uses a laser beam with constant output and a long source service life. Its disadvantages are lower printing speed, less sharp edges and limited accuracy for fine details.
DLP (projector technology) cures an entire layer at once. It offers a sharp image, uniform backlighting, constant light output and a long light source service life. This makes it suitable for precise and repeatable production, particularly in professional applications.
LCD technology is affordable and allows multiple objects to be printed at once, but suffers from fluctuating light output, uneven backlighting and a shorter display service life, which limits its long-term stability. It is therefore more suitable primarily for hobby use or for more experienced users who can compensate for these limitations when setting up the process.
MJP (inkjet nozzles) offers high accuracy and speed, but at the cost of higher operating costs, a limited range of materials and lower mechanical resistance of the printed parts.
Buoyancy and Layer Thickness Control: A Key Difference Between Technologies
One of the most important physical phenomena in resin 3D printing is buoyancy, which arises when the material is compressed. This phenomenon is unavoidable and affects all bottom-up projection technologies, regardless of the manufacturer or type of equipment.
The difference between individual systems, however, lies in how buoyancy is controlled. Basic machines operate with fixed timing settings and assume ideal process conditions. In practice, however, situations can arise where the actual layer thickness does not match the set parameters.
| Fig 3. Action of forces |
More advanced 3D printers are therefore equipped with intelligent layer thickness sensors and feedback, which make it possible to monitor the actual state of the process in real time and respond to deviations. This makes it possible to actively compensate for the forces arising, prevent uneven curing of individual layers and achieve a homogeneous material structure throughout the full height of the part.
This is where the difference between a hobby solution and a professional manufacturing technology becomes most evident.
The Importance of Uniform Backlighting and Light Output Control
Another crucial factor affecting the quality of resin 3D printing is the uniformity of backlighting across the entire build area. If the light source does not provide constant and homogeneous output, differences arise in the degree of curing in individual areas of the layer.
These differences subsequently affect not only dimensional accuracy, but also the mechanical properties and health safety of the resulting parts. While minor deviations may be negligible in simple models, they can represent a major problem in functional or precision components.
Professional machines therefore mask the light source to ensure uniform intensity across the entire build area. At the same time, they actively monitor the output of the light source and adjust curing parameters to keep the process stable even during long-term operation and with the build area fully utilised.
| Fig. 4 Difference in backlighting: 10 % for the lower class, 0.5 % for the higher class |
Light penetration, wavelength and Z-axis compensation
Curing quality is also significantly influenced by the wavelength of the UV light used. Technologies operating at a wavelength of 385 nm allow more precise control of polymerisation and reduce unwanted light penetration through the material along the Z axis. This makes it possible to achieve sharper edges, better detail definition and greater dimensional accuracy.
| Fig. 5 The thread in the lower image no longer needs to be re-cut (cleaned up) |
By contrast, systems using 405 nm exhibit greater light scattering, which can lead to less precise curing, particularly in fine structures. For this reason, Z-axis compensation is a key element of professional solutions, especially when producing functional and precision parts. This effect is most pronounced in denser and more durable materials, particularly resins with additives, materials safe for human health, and white or transparent variants.
| Fig. 6 The glossy cytotoxic material must be removed for the printed part to fit |
Open systems and working with materials
An open system allows users to work with a wide range of materials from various manufacturers, supports innovation and gives users technological independence. However, such systems also place greater demands on operator knowledge, correct print profile settings and an understanding of how individual resins behave during curing.
Without validated 3D printing profiles and experience, an open system can lead to inconsistent results. The material profiles that manufacturers often supply with mid-range 3D printers generally contain only basic exposure timing and serve more as indicative settings, as each machine may differ in design, calibration and component ageing. Parameters therefore often need to be fine-tuned, and we will be happy to help you with this as part of our training. In the lower class, these profiles are often missing entirely and need to be created.
The situation is different for professional higher-end systems equipped with sensors. A 3D printer that actively checks that layer height is maintained ensures complete polymerisation (for example, completion of bonding). It also ensures stable environmental conditions, so material profiles can also include shrinkage compensation and other corrections to achieve accurate and repeatable geometry.
| Fig. 7 Microscopic image of the surface of a 3D-printed part along the Z axis |
Material processability and the importance of temperature
Modern resins intended for professional and medical applications are often more mechanically resistant and more viscous, placing greater demands on process control. Active heating of the material reduces resin viscosity, improves its flow and contributes to more consistent results across the entire build area.
An integral part of the process is also controlled post-curing, which has a major influence on the final mechanical properties and long-term stability of parts. In professional solutions, this step is optimised in relation to the technology used and the wavelength of the light.
Differences between classes of resin 3D printers
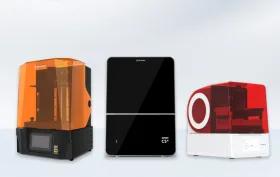
In practice, not only the technology itself but also the level of engineering of individual machines varies significantly. Resin 3D printers can be broadly divided into three basic categories.
Hobby machines (typically up to around 25 000 Kč) generally use a 405 nm light source and operate without optimised material profiles. Exposure stability may fluctuate, cooling is often limited, and the design is predominantly mechanical, without sensors for process monitoring. These machines have lower accuracy, require frequent calibration of printing parameters and typically have a service life of around two years.
Mid-range machines (up to around 150 000 Kč) often already use LCD systems with a wavelength of 385 nm and more stable illumination thanks to better cooling. Nevertheless, they generally lack sensors that monitor printing progress, so the process is still based primarily on mechanical movement. They require less frequent calibration and their typical service life is approximately five years.
Higher-end professional machines are usually projector-based systems operating at 385 nm, equipped with sensors that monitor printing progress and light source output. As a result, they can actively stabilise the process and achieve high accuracy and production repeatability. Their service life can reach up to 15 years, and ready-made material profiles enable reliable printing without the need for complex calibration.
| Fig. 7 Lower-class, mid-range and higher-end 3D printers |
Why local technical support is crucial
In the long-term operation of resin 3D printing, it is not only the 3D printer itself that matters, but above all the ability to consistently control, optimise and maintain the entire process over the long term. A key role here is played by a local technical partner who understands not only the technology, but also its physical limitations and practical deployment in production.
At cotu, we approach resin 3D printing as a comprehensive manufacturing process, not as an isolated technology. We provide technical support, material selection, process optimisation and the transfer of know-how from real industrial and medical applications.
We help customers not only select and implement new technology, but also make effective use of the machines they already have in their company – even if they were not purchased directly from us. We support them in process setup, production validation and long-term operation – from development through prototypes to stable small-batch production.
Resin 3D printing offers high accuracy and flexibility, but its true potential is only realised when the entire manufacturing process is properly controlled. It is precisely in long-term operation and under higher quality requirements that technological details, control of physical phenomena and expert know-how make the difference – not just the machine's catalogue specifications.
Would you like resin 3D printing to work reliably in your operation too?
Get in touch with us and we will discuss how to set up the technology and process to deliver stable results, high quality and real manufacturing value.
Suppliers on this topic
-

3D Tlač - Stepanek3D
3D scanning, 3D printing, editing of 3D models, plastic atypes, custom production, small series production, production… -

LukMatic s.r.o.
LukMatic is a modern Czech company that has been providing professional services in the field of additive… -
SORTEC EUROPE, s. r. o.
Supply of robotic systems for large-format pellet 3D printing, custom 3D printing of parts up to 3 m, mould… -
FilamentyBrno.cz
Custom 3D printing, filaments and 3D printer servicing. Prototypes, jigs and small series for companies in Brno. -

ADATEX, s.r.o.
3D printing, 3D printers, 3D scanners, 3D scanning and inspection, 3D digitization, 3D measurement, 3D model, 3D… -

OSMOS s.r.o.
ERP software, 3D design of plastic products, simulation of plastic injection, plastic press, plastic injection…



INOFEST 2026: A car manufacturer and a vineyard face the same challenges. Nitra made that clear
5.10.2026 On 29 September, the Creative Centre of the Slovak University of Agriculture in Nitra hosted the seventh edition of the INOFEST innovation festival. The event brought together 164 participants and featured 28 speakers, 53 companies, and 16...
Most read in the last 7 days
-
Polymer prices - october price increases partly successful, with minor corrections expected in the week ahead
-
Polymer prices – the increase in olefin monomer contract prices in October was in line with expectations
-
Plastica-expo 26
-
Long-lasting solution: Radiation-crosslinked PE-Xc pipes for drinking water supply
-
Polymer prices - Year-End Polymer Price Scenarios






Most read in the last 7 days
-
Polymer prices - october price increases partly successful, with minor corrections expected in the week ahead
-
Polymer prices – the increase in olefin monomer contract prices in October was in line with expectations
-
Plastica-expo 26
-
Long-lasting solution: Radiation-crosslinked PE-Xc pipes for drinking water supply
-
Polymer prices - Year-End Polymer Price Scenarios





